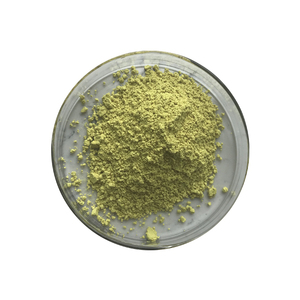
In the highly regulated global nutraceutical, pharmaceutical, and functional food sectors, securing reliable CE Certified Active Ingredient Factories is paramount for batch consistency, regulatory compliance, and consumer safety. High-purity botanical actives, such as Quercetin (CAS 117-39-5) derived from Sophora Japonica L., represent core anti-inflammatory, antioxidant, and senolytic ingredients demanded across North America, Europe, and Asia-Pacific markets.
Direct factory-grade standardized botanical extracts, liposomal formulations, and high-purity monomers for B2B procurement.
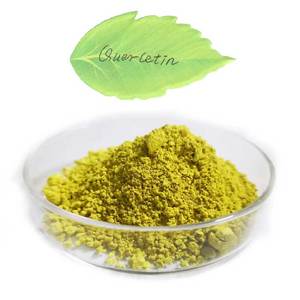
Bridging raw botanical extraction with modern pharmaceutical precision and rigorous global quality management systems.
Operating under strict GMP compliance, our state-of-the-art production base holds ISO, HALAL, KOSHER, and Organic certifications. Every production line undergoes annual independent safety audits to guarantee zero cross-contamination and audit-ready documentation.
Utilizing solvent-free Supercritical CO2 extraction technology alongside enzymatic and low-temperature vacuum drying, we preserve thermal-sensitive bioactive compounds while driving organic solvent residue far below strict EU and FDA limit thresholds.
Every single export lot travels with a batch-specific Certificate of Analysis. Our internal testing center, equipped with HPLC, GC-MS, UV-Vis, and Atomic Absorption Spectrometry, provides full assay profiles, heavy metal testing (<10ppm), and pesticide screening.
Through our contracted raw material planting bases in verified geographical zones, we record full cultivation, harvest date, and drying parameter logs. Our lot numbers track finished powder directly back to the specific agricultural farm lot.
We provide tailormade active ingredient solutions including micro-encapsulated liposomal powders, custom mesh sizing (from 80 to 200 mesh), customized bulk densities, and specialized organic-compliant carrier systems (such as maltodextrin or rice starch).
Maintaining rolling stock of core active ingredients like Quercetin Anhydrous, Dihydrate, and Saffron Actives in humidity-controlled warehouses ensures immediate shipment within 3–5 business days, supported by complete customs clearance packages.
| Analytical Parameter | Quercetin Dihydrate 95% | Quercetin Anhydrous 98% | Liposomal Quercetin 50% | Testing Method |
|---|---|---|---|---|
| Active Assay Content | ≥ 95.0% Quercetin | ≥ 98.0% Quercetin | ≥ 50.0% Encapsulated | HPLC-DAD (USP/EP) |
| Loss on Drying | 10.0% - 14.0% | ≤ 4.0% | ≤ 5.0% | GB 5009.3 / USP <731> |
| Heavy Metal Limits | Pb < 2ppm, As < 1ppm | Pb < 1ppm, As < 1ppm | Pb < 1ppm, As < 0.5ppm | ICP-MS (EU 2023/915) |
| Solvent Residue | Ethanol < 5000 ppm | Ethanol < 3000 ppm | Solvent Free Process | Headspace GC-FID |
| Microbiological Count | TAMC < 1000 cfu/g | TAMC < 1000 cfu/g | TAMC < 500 cfu/g | USP <2021> Compliant |
Analyzing market structural shifts, stringent regulatory evolution, and high-gain procurement strategies for global supply directors.
Global pharmaceutical and supplement brand owners are rapidly shifting procurement criteria from cost-per-kilo to environmental compliance and solvent safety. Conventional extraction relying on toxic organic solvents (such as dichloromethane or high residual methanol) is being phased out under EU REACH standards. Suppliers operating zero-solvent Supercritical CO2 fluid extraction and membrane isolation processes are receiving preferred vendor status due to reduced carbon footprints and non-detectable residual solvent risk profiles.
Enforcement of updated contaminants regulations (such as EU Regulation 2023/915 and stringent California Proposition 65 limits) requires active ingredient factories to implement advanced purification lines. Procurement officers must verify that active plant powders undergo validated sterilization—such as gamma-free steam sterilization—ensuring absolute non-detection of Ethylene Oxide (EtO) and 2-Chloroethanol, alongside rigorous ICP-MS testing for Lead, Cadmium, Mercury, and Arsenic.
Geopolitical shifts and climate-driven yield fluctuations in raw agricultural botanical biomass (e.g., Sophora Japonica flower buds or saffron crocus) have highlighted the vulnerability of buying through middle-tier trading desks. Strategic procurement teams are forming direct supply partnerships with integrated primary manufacturers like RAAG Biotech, securing multi-year volume contracts backed by reserve batch stockpiles to insulate against price volatility.
The modern quality assurance qualification workflow demands instant access to comprehensive compliance dossiers. Suppliers are expected to deliver audit-ready documentation packets—including raw material geographical coordinates, HPLC assay chromatograms, allergen declarations, BSE/TSE certificates, and non-GMO affidavits—with digital QR validation directly attached to shipping drums.
How advanced particle engineering and biotransformation are revolutionizing flavonoid bioavailability and functional efficacy.
Natural flavonoids like standard Quercetin exhibit low aqueous solubility and limited intestinal absorption (<2%). Industry R&D is heavily focused on Liposomal Encapsulation Technology. By surrounding active Quercetin molecules with a phospholipid bilayer matrix (50% active loading), cellular uptake increases up to 8 to 20 times compared to unformulated crystalline powders, unlocking superior efficacy in cellular health, senolytic therapy, and sports performance supplements.
Traditional chemical hydrolysis is increasingly replaced by green enzymatic conversion processes. Bio-enzymatic treatment allows precise cleavage of rutin glycosides into pure Quercetin Anhydrous without degrading active molecular rings. This yields purities exceeding 98.0% by HPLC while generating zero toxic chemical waste byproducts, perfectly matching pharmaceutical precursor requirements.
To support ready-to-drink (RTD) beverage mixes, stick packs, and effervescent delivery forms, active ingredient factories are engineering ultrafine micro-granules (100 to 200 mesh) and self-emulsifying delivery systems (SEDDS). These physical particle modifications prevent sediment precipitation, improve powder flowability during high-speed capsule filling, and maintain dispersion stability in liquid formats.
Direct technical answers addressing regulatory files, analytical testing, batch consistency, and minimum order requirements.
Every commercial batch is delivered with a complete quality packet including a batch-specific COA (verifying HPLC assay, loss on drying, ash content, heavy metals, pesticides, and microbiological counts), MSDS, Technical Data Sheet (TDS), Specification Sheet, Process Flowchart, Non-GMO Statement, Allergen Declaration, and Ethylene Oxide (EtO) Free Certificate. Third-party testing via SGS or Eurofins can be pre-arranged upon request.
Quercetin Dihydrate contains two bound water molecules within its crystalline lattice, typically resulting in a moisture content (loss on drying) of 10% to 14% and an active assay of around 95%. Quercetin Anhydrous undergoes specialized thermal vacuum drying to remove bound water, achieving a moisture content under 4.0% and an active assay of ≥98.0%. Anhydrous forms are preferred for moisture-sensitive hard capsule and tablet formulations.
We source raw Sophora Japonica buds exclusively from contracted GAP-compliant planting bases away from industrial zones. Raw biomass undergoes rigorous intake testing. Our extraction facility utilizes multi-stage filtration and columns that isolate pure flavonoid compounds while removing trace heavy metals, ensuring final lead, arsenic, cadmium, and mercury levels remain well below EU and USP regulatory thresholds.
Our standard wholesale MOQ for stock active ingredient powders (such as Quercetin 95% / 98%) is 25 kg (one fiber drum with double PE inner bags). For specialized pilot trials, analytical validation, or formulation R&D, we supply small sample packages from 1 kg up to 5 kg, complete with retained sample COAs.
Yes. RAAG Biotech operates in-house particle engineering systems. We can customize particle sizes from coarse granules (for direct compression tablets) down to micronized 200-mesh powders (for rapid dispersion), adjust bulk density, or formulate specialized carriers (such as liposomal phospholipid matrices) to match your precise manufacturing equipment needs.
When stored in unopened original fiber drums in a cool, dry place away from direct sunlight and heat (temperatures below 25°C and relative humidity below 60%), our standardized botanical extracts maintain a verified shelf life of 24 to 36 months. Accelerated and real-time stability test reports are available for qualified pharmaceutical and nutraceutical buyers.
Request batch-specific COAs, request free technical sample kits (10g–50g), or consult with our senior phytochemical engineers for custom specification development.
Inquire Now