Supercritical CO2 Lines
Operates solvent-free CO2 extraction for lipophilic compounds, volatile oils, and carotenoid fractions without thermal denaturation.
Equipped with state-of-the-art production machinery, comprehensive analytical inspection instruments, advanced purification systems, and a highly trained technical team, [email protected] guarantees the production of standardized, consistent, and pure botanical extracts. By upholding rigorous cGMP standards at every stage of processing, we serve international dietary supplement, pharmaceutical, and cosmetic formulation buyers with batch-to-batch reliability and complete traceability.
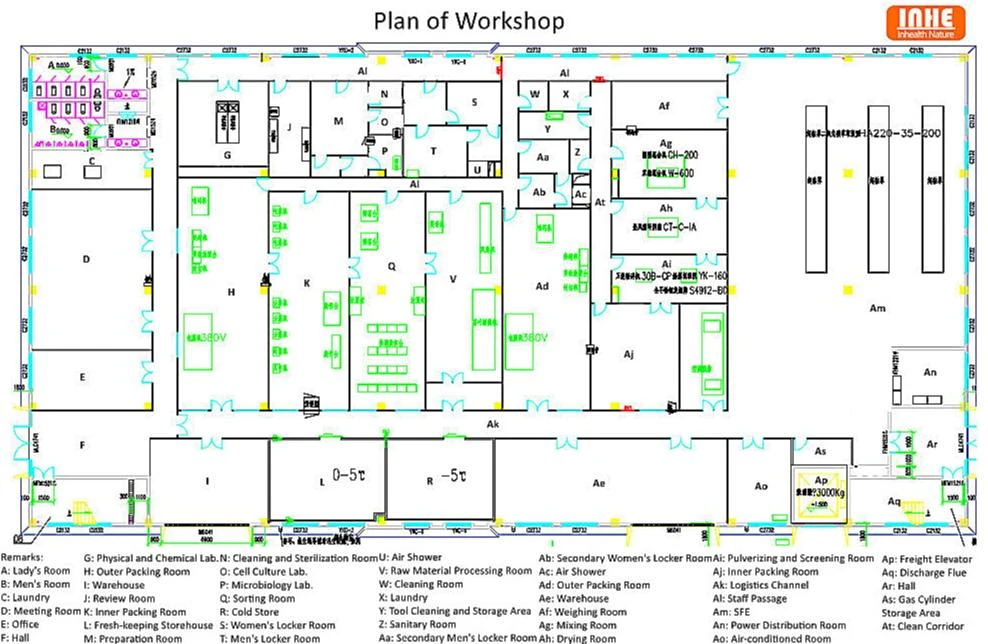
Our modern extraction workshop is engineered to optimize processing parameters across varied botanical raw materials. From initial raw herb pretreatment to solvent extraction and concentration, every phase is continuously logged against strict Standard Operating Procedures (SOPs).
The facility features automated control systems that maintain precise temperature, pressure, and solvent ratio parameters, ensuring maximum active marker recovery while minimizing thermal degradation of heat-sensitive compounds.
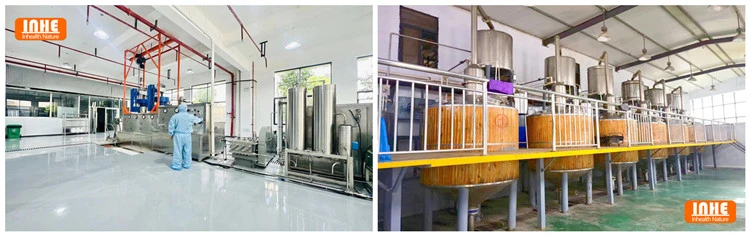
[email protected] invests continuously in leading extraction and drying infrastructure, including multi-function stainless steel extraction tanks, low-temperature vacuum concentration units, spray drying towers, and continuous counter-current extraction lines.
Our solvent-free Supercritical CO2 extraction units enable high-yield isolation of lipophilic actives and essential oils without chemical solvent residues, delivering clean-label ingredients for global formulation requirements.
Operates solvent-free CO2 extraction for lipophilic compounds, volatile oils, and carotenoid fractions without thermal denaturation.
Concentrates liquid extracts under vacuum to preserve marker potency and active compound bioactivity prior to final drying.
Converts concentrated botanical solutions into fine, uniform powders with customized particle size, bulk density, and instant solubility.
Quality assurance is embedded in our manufacturing culture. Our in-house quality control center operates advanced analytical equipment including High-Performance Liquid Chromatography (HPLC), Gas Chromatography (GC-MS), and UV-Vis Spectrophotometers.
Every raw material batch and finished production lot undergoes stringent testing for active assay percentage, heavy metals (Pb, As, Cd, Hg), pesticide residues, residual solvents, and microbiological safety prior to QA batch release.
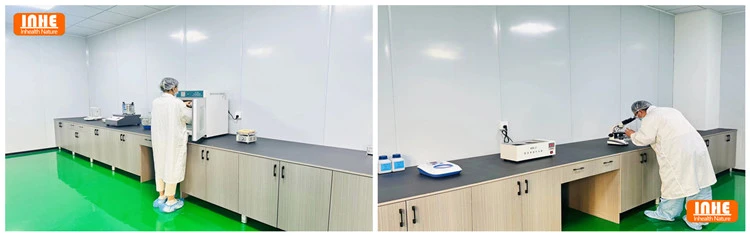
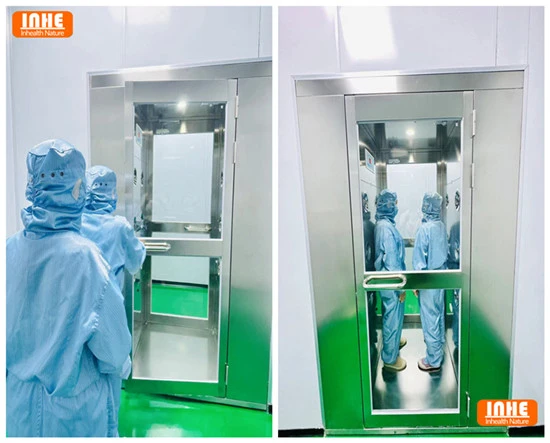
To produce single-monomer plant extracts and high-purity active markers, [email protected] utilizes preparative column chromatography, industrial-scale resin separation, and membrane filtration technologies.
This specialized purification platform allows us to isolate target plant compounds (such as Crocin, Crocetin, and Hirudin fractions) up to 98%+ purity levels, satisfying demanding pharmaceutical and clinical nutra standards.
Separates complex herbal matrices into target purified fractions and high-assay monomer compounds.
Removes micro-impurities and clarifies extracts under gentle physical separation conditions.
Staffed with experienced chemical engineers, phytochemists, and QA personnel managing end-to-end operational execution.
Our technical team provides full factory qualification documentation, process flow charts, ISO/HALAL/KOSHER certs, and COAs for international procurement audits.
Get a Quote