HPLC Grade
Explore our export-grade, HPLC-verified raw materials manufactured under strict ISO/GMP quality management systems with full CE compliance files.
Operating state-of-the-art bioprocessing plants to supply European and global pharmaceutical brands with certified raw materials.
The modern bio-pharmaceutical and high-end nutraceutical sectors demand an unprecedented level of chemical consistency and biological activity. As premier CE Certified Peptide Powder Manufacturers, RAAG Biotech Co., Ltd. bridge the critical gap between raw agricultural inputs and pharmaceutical-grade active ingredients. Our industrial processing platforms combine traditional enzymatic hydrolysis, subcritical water extraction, and cutting-edge supercritical CO2 extraction technologies to yield bioactive fractions with uncompromised therapeutic potential.
In peptide synthesis and botanical extraction, controlling molecular mass distribution and secondary metabolite stability is essential. For instance, in our standardized Sophora Japonica flower processing line for Quercetin Dihydrate and Quercetin Anhydrous, precise enzymatic cleavage and low-temperature membrane concentration prevent the thermal degradation of polyphenolic rings. This guarantees a verified HPLC assay profile exceeding 98% purity, adhering strictly to European Pharmacopoeia (Ph. Eur.) standards and CE compliance framework directives.
Furthermore, our dedicated bio-monomer isolation lines utilize multi-stage column chromatography and continuous recrystallization processes. By eliminating trace solvent residues (ethanol, ethyl acetate) down to parts-per-million (PPM) thresholds far below stringent ICH Q3C guidelines, we provide global formulators with raw materials that integrate seamlessly into complex parenteral, oral tablet, or advanced capsule formulations.
Founded in 2014, RAAG Biotech operates an advanced 12,000 m² GMP-compliant cleanroom facility equipped with high-performance liquid chromatographs (HPLC), UV-Vis spectrophotometers, GC-MS residual solvent analyzers, and ICP-MS heavy metal detection units.
Our fully integrated raw material sourcing network spans over 1,500 hectares of contracted GAP (Good Agricultural Practices) planting bases, ensuring 100% batch traceability from seed and soil chemistry to finished export drums.
The global market for active pharmaceutical ingredients (APIs), functional nutritionals, and cosmeceutical peptides is undergoing a seismic shift. Procurement directors across North America and the European Union are pivoting away from uncertified brokers toward direct-from-factory partnerships with verified CE certified peptide powder manufacturers. Key macroeconomic and technical drivers shaping upcoming procurement cycles include:
| Ingredient Parameter | Standard Crude Extract | Standardized Bioactive (RAAG) | Liposomal Encapsulated Grade | Compliance Standard |
|---|---|---|---|---|
| Assay Purity (HPLC) | 10% - 40% Active | 95.0% - 98.5% Active | 50.0% Bio-Active Complex | USP / Ph. Eur. Grade |
| Water Solubility | Poor / Lipophilic | Medium Dispersibility | High Aqueous Stability | In-Vitro Dissolution Tested |
| Heavy Metal Limits | < 10.0 ppm Lead/Cadmium | < 2.0 ppm Strict Limit | < 1.0 ppm Ultra-Pure | ICP-MS Verified |
| Microbiological Count | < 10,000 cfu/g | < 1,000 cfu/g | < 500 cfu/g Pathogen Free | ISO 22000 / HACCP |
| CE & EU Documentation | Basic COA Only | Full Technical Dossier + MSDS | Complete Formulation File | CE Certified Facility |
Combining rigorous science, modern extraction infrastructure, and transparent trade terms for corporate procurement teams.
Every single batch travels with an audit-ready document package: COA (HPLC/UV assay), MSDS, allergen sheets, GMO-free certificates, and third-party heavy metal/pesticide screening from SGS or Eurofins upon request.
Need specific bulk density for high-speed tableting or water-soluble carrier options like maltodextrin, gum arabic, or sunflower lecithin? Our R&D pilot line optimizes physical parameters prior to commercial scale-up.
Our internal lot mapping links every kg of finished extract directly back to agricultural planting bases, recording harvest season, drying temperature, and zero-pesticide application histories.
Our eco-friendly CO2 extraction lines operate at precise pressures and low temperatures, isolating heat-sensitive monomers and oleoresins without toxic organic solvent residues.
We maintain rolling stock of core standardized items. Free 10g–50g lab evaluation samples ship internationally within 48 hours, supported by dedicated customs clearance specialists.
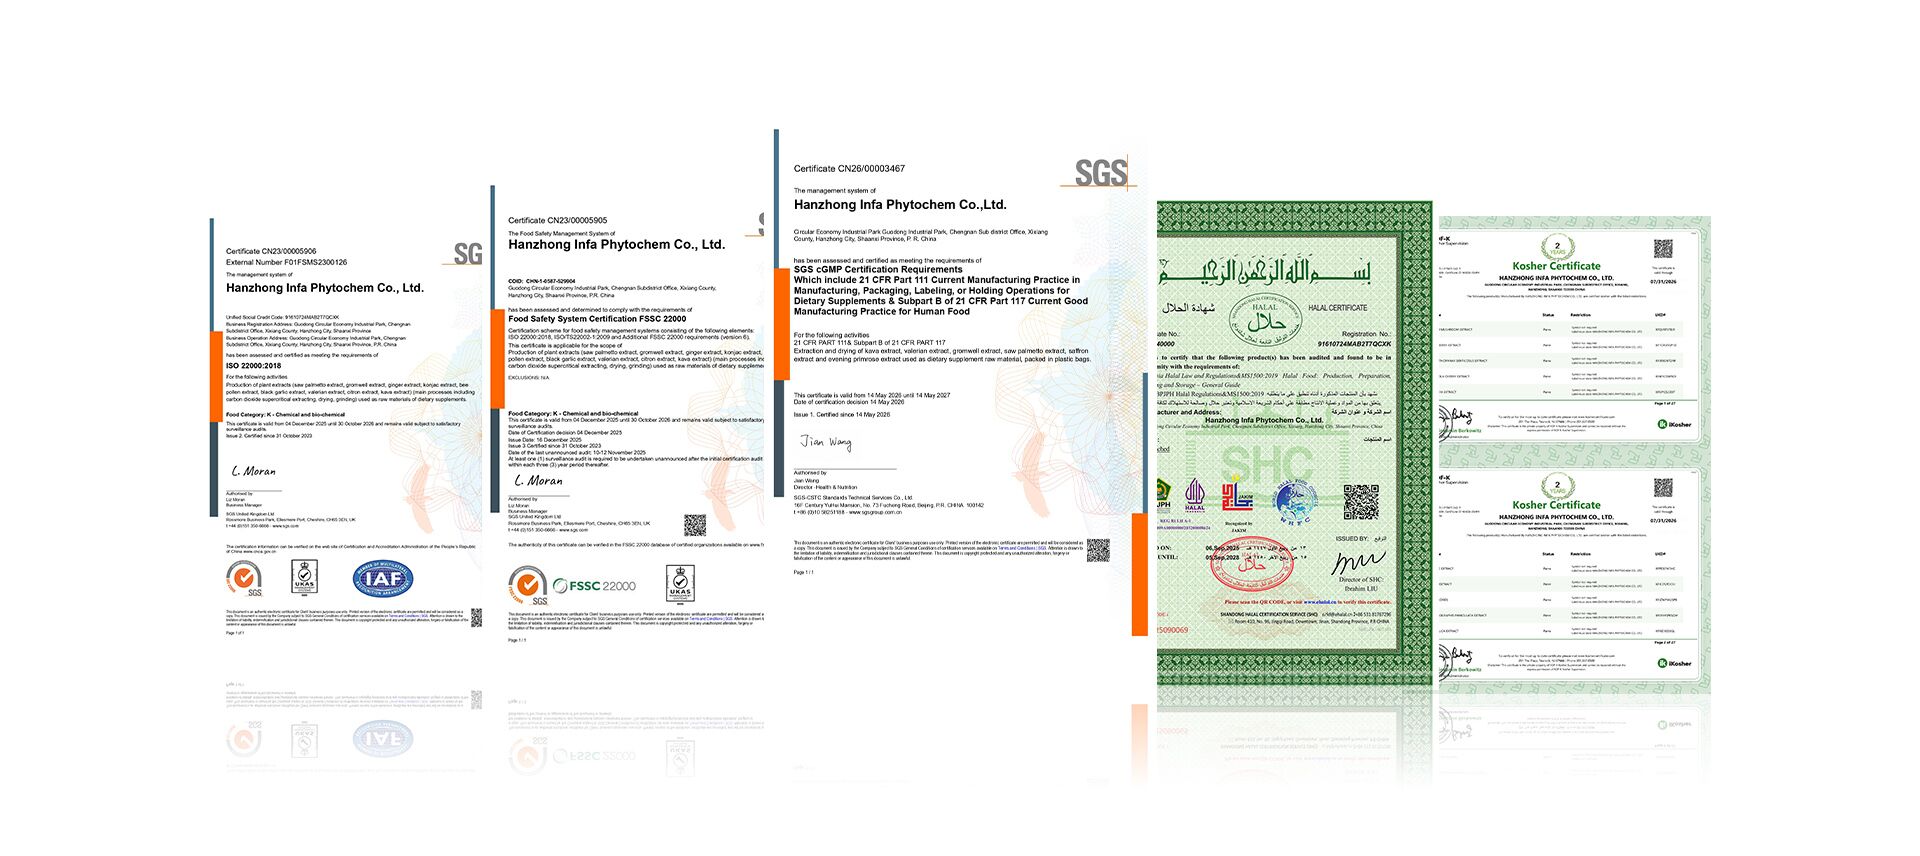
Our facilities are certified under ISO9001, ISO22000, HALAL, KOSHER, and organic standards, giving your compliance team immediate confidence during vendor qualification.
Our manufacturing protocols align with international regulatory expectations, accelerating your market entry.
Direct technical answers to clarify regulatory, logistics, and quality assurance inquiries.
Connect with our senior technical specialists. Receive tailor-made specifications, sample dispatch, and factory-direct commercial quotes within 12 hours.