Explore our export-ready, standardized fruit extract powders, oleoresins, freeze-dried preparations, and industrial processing machinery manufactured under cGMP and ISO22000 standards.
The global demand for standardized plant extracts, natural fruit powders, and purified active monomers has undergone a fundamental structural shift. Modern formulators across the nutraceutical, functional food, beverage, and pharmaceutical sectors no longer search merely for crude botanical derivatives. Today's procurement mandates demand precise active compound quantification (via HPLC, GC-MS, or UV-Vis), strict heavy metal and solvent residue compliance (conforming to USP/EP monographs), and absolute agricultural batch-level traceability.
As a leading China Best Fruit Extract Manufacturer & Supplier, RAAG Biotech Co., Ltd. operates at the intersection of modern bio-engineering and sustainable agronomy. Founded in 2014, our facility has shifted the paradigm from traditional hot-water maceration to advanced green processing technologies—including Supercritical Fluid Extraction (SFE-CO₂), low-temperature vacuum reflux, membrane filtration, column chromatography purification, and freeze-drying (lyophilization).
Information Gain Metric: Standard fruit juice concentrates often suffer from thermal degradation of heat-sensitive compounds (such as L-ascorbic acid, anthocyanins, and volatile esters). Advanced subcritical and freeze-drying methodologies preserve up to 96.4% of native bioactive phytochemicals while maintaining water activity (aw) below 0.30 for prolonged ambient stability.
By controlling contracted planting bases across specialized micro-climates in China, we ensure that raw agricultural inputs—ranging from sea buckthorn berries harvested in high-altitude cold regions to pomegranate, grapefruit, and capsicum crops—are cultivated under controlled pesticide regimes. This guarantees that every bulk drum dispatched to international buyers arrives with an audit-ready technical file, complete Certificate of Analysis (COA), MSDS, Allergen Statement, and Non-GMO Declaration.
Our 10,000 square meter GMP-certified manufacturing infrastructure utilizes specialized processing lines engineered to process diverse botanical matrices without compromising cellular integrity or chemical potency.
Operates without organic solvents, using dense phase CO₂ at critical pressure and temperature. Ideal for lipophilic fruit oils, capsicum oleoresin, and lipid-soluble antioxidants, producing zero solvent residues.
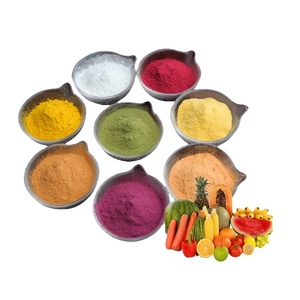
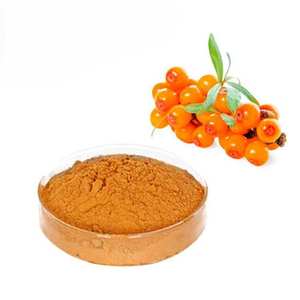
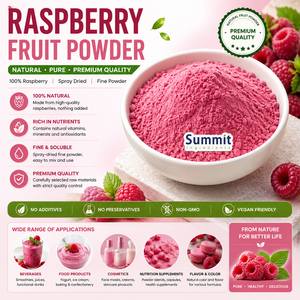
Sublimates ice directly to vapor under ultra-low temperatures and vacuum conditions. Preserves delicate flavor profiles, enzymatic activity, and heat-fragile vitamins in fruit powders like raspberry and sea buckthorn.
Utilizes macroporous resin and column chromatography to isolate target plant monomers to purities exceeding 98%. Enables production of high-grade crocin, crocetin, and specific flavone compounds.
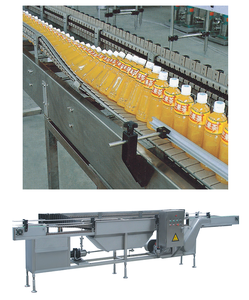
In addition to raw ingredient extraction, our engineering capabilities extend to full industrial juice production line manufacturing (such as our KANGDELI automated lines). This dual expertise in both equipment engineering and biochemical processing provides us with deep insight into continuous liquid-solid extraction, enzymatic clarification, flash pasteurization, and aseptic filling systems.
To assist global procurement officers and formulation scientists in evaluating raw material performance, the table below delineates key technical parameters across our primary product platforms.
| Product Category | Primary Processing Method | Active Marker / Assay Standard | Water Activity (aw) / Moisture | Solubility Profile | Primary Regulatory Compliance |
|---|---|---|---|---|---|
| Standardized Fruit Extracts | Water/Ethanol Reflux + Spray Drying | Total Polyphenols > 30-50% (UV/HPLC) | aw < 0.35 | Moisture < 5.0% | 100% Water Soluble | USP / EP / ISO |
| Supercritical CO₂ Oleoresins | Supercritical Fluid Extraction (SFE) | Capsaicinoids / Lipophilic Actives | Lipid Matrix (Zero Moisture) | Oil Dispersible / Fat Soluble | Solvent-Free Clean Label |
| Freeze-Dried Fruit Powders | Low-Temp Lyophilization (-40°C) | Native Vitamin C & Anthocyanins | aw < 0.25 | Moisture < 3.0% | Dispersible / Reconstitutable | Organic / Non-GMO |
| Purified Plant Monomers | Multi-Stage Column Chromatography | Pure Monomer > 95% - 99% (HPLC) | Crystalline Powder (< 1.0%) | Solvent Specific (Methanol/Water) | Pharma Grade Standard |
| Liquid Extract Concentrates | Liquid-Solid Countercurrent Extraction | Brix 60-65° Standardized | Liquid Concentrate | Fully Miscible Liquid | Food Grade / Beverage |
As international supply chains face evolving regulatory hurdles and changing consumer demands, B2B procurement strategies for fruit extracts are rapidly transforming. Purchasing departments must align with suppliers capable of navigating three macro trends:
Regulatory agencies such as the European Food Safety Authority (EFSA) and US FDA are continually lowering acceptable thresholds for organic solvent residues (such as hexane, dichloroethane, and ethyl acetate). Future procurement heavily favors manufacturers utilizing ethanol-water ratios or supercritical CO₂ systems that yield zero synthetic toxic residues.
Raw fruit polyphenols often exhibit low stability when exposed to light, heat, or low pH stomach environments. Advanced manufacturers are adopting spray-drying microencapsulation using carrier matrices like maltodextrin, gum arabic, or liposomal phospholipid complexes (e.g., Silybin Phospholipids) to significantly improve intestinal absorption and shelf-life stability.
Global brand owners can no longer afford supply chain disruptions due to pesticide contamination or heavy metal spikes (Lead, Cadmium, Arsenic, Mercury). Contracting directly with audited planting bases in China allows continuous monitoring of soil quality, irrigation water purity, and harvest timing, backed by LC-MS/MS 400+ multi-residue pesticide screens.
Supply Chain Insight: Sourcing directly from a direct manufacturer rather than trading intermediaries reduces lot-to-lot color variability by up to 40% and ensures direct access to retain samples for regulatory cross-checking during customs clearance.
At RAAG Biotech, every single production batch undergoes standardized testing protocols before receiving quality control sign-off. Our quality control lab is equipped with high-performance liquid chromatography (HPLC) with diode-array detection (DAD), gas chromatography-mass spectrometry (GC-MS), atomic absorption spectroscopy (AAS), and rapid microbiological testing equipment.
Assay validation ensures active marker levels (e.g., Safranal, Crocin, Valerenic Acid, Bioactive Organic Acids) precisely match client specifications across every batch.
Mesh size testing (80-120 mesh), bulk density, tap density, moisture content, and water activity ($a_w$) determination prevent clumping during high-speed encapsulation.
Total Viable Count (TVC), Yeast & Mold, E. Coli, Salmonella, and Staphylococcus aureus screening ensure 100% food and pharmaceutical grade compliance.
Partner with a proven China Fruit Extract Manufacturer. Contact our technical sales engineering team today to receive detailed batch COAs, custom pricing matrices, and sample dispatches tailored to your formulation needs.
Get a Quote