Water-Extracted Naringin Powder: Over 98% Purity, Heavy Metal Free
Purity: ≥ 98% (HPLC)
Extraction: 100% Water Solvents
Grade: Pharma / Food Grade
Direct factory supply manufactured in GMP-certified and ISO-audited cleanrooms. Complete with batch-specific HPLC/UV/GC COAs, heavy metal profiles, pesticide residue screenings, and DMF technical files.
As a premier Chinese manufacturer established in 2014, RAAG Biotech integrates specialized botanical extraction, column chromatography monomer purification, and medical-grade mineral refinement to serve over 300 B2B enterprise clients worldwide.
Our manufacturing infrastructure is fully ISO22000, HACCP, HALAL, KOSHER, and GMP audited. Every single production lot undergoes rigorous multi-stage analytical releasing protocols before export clearance.
Operating state-of-the-art Supercritical CO2 extraction, water and steam hydro-distillation, enzymatic hydrolysis, and low-temperature membrane concentration to maximize active marker purity while controlling thermal degradation.
Every export order is accompanied by comprehensive CoA (HPLC/UV assay), MSDS, TDS, Allergen Statements, GMO-free certifications, residual solvent analysis (ICH Q3C), and full heavy metal panels.
Raw botanical inputs originate from contracted GAP (Good Agricultural Practices) growing bases across China. Full lot coding enables tracing finished extracts back to field origin, harvest date, and soil testing logs.
In-house laboratory team capable of adjusting bulk particle mesh size (up to 1250 mesh fine powders), carrier systems (maltodextrin, gum arabic, starch-free), water-solubility profiles, and custom assay concentrations.
Rolling inventory maintained for core active ingredients. Fast dispatch within 3-5 business days for stock items, with complete customs clearance support for air, sea, and express international freight destinations.
The global pharmaceutical and nutraceutical raw material market is experiencing an unprecedented structural shift. Procurement officers, pharmaceutical formulation scientists, and supply chain directors are rapidly recalibrating their sourcing strategies to align with heightened global regulatory scrutiny, tighter environmental compliance, and an urgent requirement for total supply chain transparency. As a premier China wholesale pharmaceutical ingredient supplier & exporter, RAAG Biotech stands at the epicenter of this industrial evolution, offering high-purity active pharmaceutical ingredients (APIs), botanical extracts, functional amino acids, and high-performance mineral excipients.
China’s position as a critical node in global pharmaceutical manufacturing is no longer merely defined by cost efficiency. Over the past decade, substantial capital investments in green chemistry, continuous-flow synthesis, chromatographic purification, and automated quality control have transformed Chinese manufacturers into technology-driven centers of excellence. International buyers from North America, Europe, the Middle East, and Southeast Asia are increasingly leveraging China’s robust industrial ecosystem for both high-volume standardized ingredients and specialized high-purity monomer compounds.
However, modern international procurement demands far more than basic chemical synthesis or crude extraction. Today’s market requires strict compliance with United States Pharmacopeia (USP), European Pharmacopoeia (EP), and British Pharmacopoeia (BP) standards, alongside comprehensive documentation for impurity profiling (ICH Q3A/B), residual solvent control (ICH Q3C), and elemental impurity limits (ICH Q3D). Suppliers who fail to provide comprehensive technical dossiers are quickly eliminated from global supply networks.
To illustrate the technical depth required by modern B2B buyers, let us examine the specialized manufacturing parameters of key ingredient groups currently exported by leading Chinese suppliers:
The following matrix outlines the analytical specifications, testing methodologies, and regulatory compliance standards maintained across our core product offerings:
| Ingredient Category | Standard Grade / Purity | Testing Methodology | Key Quality Control Focus | Global Compliance |
|---|---|---|---|---|
| Naringin Powder | ≥ 98.0% Active Flavonoid | HPLC External Standard | Zero Organic Solvent Residue, Heavy Metals < 10ppm | Pharma / Food Grade, COA, MSDS |
| Pharma Montmorillonite | 600, 1000, 1250 Mesh | XRD / Laser Particle Analyzer | Adsorption Capacity, Microbial Limit < 100 cfu/g | EP / BP / ChP Compliant |
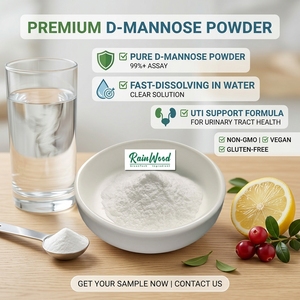
| D-Mannose Powder | 99.0% - 101.0% Pure | HPLC / Specific Rotation | Specific Optical Rotation, Transmittance > 95% | USP / FCC Standard, Kosher/Halal |
| Glycine (Pharma Grade) | ≥ 99.5% Crystalline | Titration Assay / Heavy Metals | Chloride < 0.007%, Loss on Drying < 0.2% | USP / EP Grade, Non-GMO |
| Pullulan Powder | Natural Fermentation Grade | Viscosity / Molecular Weight | Film-Forming Property, High Oxygen Barrier | Food Additive / OEM Capsule Grade |
Navigating the next decade of pharmaceutical ingredient sourcing requires a forward-looking understanding of industry trajectories. B2B purchasers must build resilient supplier relationships that account for shifting regulatory landscapes and technological breakthroughs.
Environmental regulations in importing countries (such as the EU REACH framework and FDA environmental assessments) are placing greater emphasis on the carbon footprint and chemical safety of raw material production. Traditional extraction techniques relying on harsh organic solvents (e.g., hexane, dichloromethane) are rapidly being phased out in favor of Supercritical CO2 Fluid Extraction and pure water-based isolation processes. CO2 extraction operates at lower temperatures, preserving delicate lipophilic bioactive components without leaving chemical residues, making it the preferred choice for premium nutraceuticals and pharmaceutical preparations.
Global health authorities have continuously lowered allowable limits for agricultural residues and heavy metals. Regulatory agencies now enforce strict testing panels for over 400 pesticide residues (via LC-MS/MS and GC-MS/MS), elemental impurities (Cadmium, Lead, Arsenic, Mercury via ICP-MS), and mycotoxins (Aflatoxins B1, B2, G1, G2 and Ochratoxin A). Chinese exporters capable of maintaining fully integrated agricultural supply chains and operating in-house state-of-the-art testing laboratories hold a decisive competitive advantage in global market access.
The global dietary supplement and prescription drug industries are witnessing a massive consumer-driven pivot away from animal-derived gelatins (bovine and porcine). Vegetarian and clean-label alternatives—specifically HPMC (hydroxypropyl methylcellulose) and Pullulan—are experiencing double-digit annual growth rates. Pullulan, in particular, offers superior moisture resistance and oxygen impermeability, protecting sensitive APIs and botanical compounds from oxidative degradation without requiring artificial cross-linking agents.
Active ingredients frequently suffer from poor bioavailability or inconsistent dissolution rates due to coarse particle size distributions. Modern pharmaceutical procurement increasingly specifies exact physical parameters, including bulk density, tap density, pore volume, and narrow particle size spreads (such as 600 mesh, 1000 mesh, and 1250 mesh ultra-fine powders). Customized particle engineering improves tablet compressibility, suspension stability, and intestinal absorption efficiency, eliminating formulation bottlenecks for finished dosage manufacturers.
Supply chain disruptions in recent years have compelled global procurement organizations to move away from single-source reliance and spot-market buying. Leading pharmaceutical brands now demand long-term supply contracts with enterprise-scale manufacturers who maintain multi-facility redundancy, large-scale warehousing capacity, and continuous audit readiness for international regulatory agencies.
Detailed technical and logistical answers provided by our quality control and global trade compliance departments.
Every shipment from RAAG Biotech is accompanied by a comprehensive document package including a batch-specific Certificate of Analysis (COA featuring quantitative HPLC/UV/GC assays), Material Safety Data Sheet (MSDS), Technical Data Sheet (TDS), Process Flow Chart, Allergen Statement, Non-GMO Declaration, and Residual Solvent Report conforming to ICH Q3C guidelines. Heavy metal and microbiological test reports are generated per production lot.
Batch consistency is achieved through strict standardized manufacturing protocols. Botanical raw materials are harvested from contracted GAP planting bases with recorded origin and chemical profiling. For mineral products like Bentonite and Montmorillonite, raw clay undergoes systematic wet-purification and high-precision air classification to guarantee uniform cation exchange capacity and mesh size (600 to 1250 mesh) across consecutive production runs.
Yes. Our experienced technical team offers comprehensive OEM/ODM customization. We can adjust physical parameters including mesh size fineness (from standard coarse powders to 1250 mesh superfine), bulk density, moisture content, solubility profiles (water-soluble vs. oil-dispersible), and carrier selection (maltodextrin, gum arabic, or carrier-free pure powders) based on your specific formulation requirements.
For standard active ingredients and plant extracts, our standard MOQ is 25 kg (packaged in fiber drums with double inner PE bags). For high-purity monomer reference materials, smaller MOQs starting at 1 kg are available. We readily provide 20g–50g complimentary evaluation samples accompanied by matching sample COAs for qualified international enterprise buyers.
In addition to our internal high-precision laboratory testing (equipped with Agilent HPLC, GC, and ICP-MS systems), we regularly collaborate with independent international accredited testing facilities such as SGS, Eurofins, and Pony Testing. Importers may request third-party sampling and testing prior to container loading.
Solid powders are sealed inside heavy-duty double food-grade polyethylene bags containing desiccant packs, which are then enclosed in moisture-resistant 25kg cardboard or fiber drums. For hygroscopic powders (such as D-Mannose or Pullulan), aluminum foil vacuum packaging is utilized to prevent moisture absorption and caking during ocean or air transit.
Whether you require high-purity Naringin powder, ultra-fine 1250 mesh medical grade Montmorillonite, pure D-Mannose, clean-label Pullulan, or customized OEM extraction services, our technical engineering desk is ready to support your formulation requirements.