Directly sourced, marker-standardized active ingredients and turnkey extraction machinery built to rigorous global Pharmacopoeia standards.
In the modern global supply chain, purchasing managers, formulation scientists, and regulatory officers face escalating challenges regarding ingredient identity, batch-to-batch consistency, heavy metal contamination, and residual solvent control. As Google's Search Quality Rater Guidelines emphasize E-E-A-T (Experience, Expertise, Authoritativeness, and Trustworthiness), evaluating B2B suppliers requires moving past basic price per kilogram quotes. Technical procurement demands an audit-ready evaluation of extraction methodologies, marker compound stability, and transparent supply chain integrity.
RAAG Biotech Co., Ltd. (operating since 2014) has established itself as an authoritative manufacturer and global exporter of standardized herbal extracts, pure monomers, supercritical CO₂ oleoresins, plant powders, essential oils, and fermented bio-actives. Operating out of a state-of-the-art facility in Xi'an's High-tech Zone, Shaanxi, China, RAAG Biotech bridges raw botanical harvesting with advanced industrial-scale purification.
The global concentrated botanical extract market is experiencing a structural transition driven by stricter compliance parameters from the U.S. FDA (21 CFR Part 111 cGMP), EFSA (European Food Safety Authority), and GCC regulatory authorities. Industrial buyers are prioritizing suppliers capable of issuing detailed Certificate of Analysis (CoA) packets containing high-performance liquid chromatography (HPLC), gas chromatography-mass spectrometry (GC-MS), and ultra-violet spectrophotometry (UV-Vis) validation data.
Requires high-potency standardized powders with low bulk density, tight mesh size distribution (80-120 mesh), and rapid disintegration profiles for hard capsules, softgels, and direct-compressible tablets.
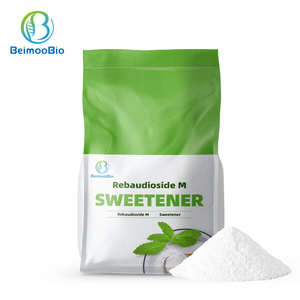
Demands 100% water-soluble liquid concentrates or micro-encapsulated spray-dried powders that offer heat stability, zero sediment yield, and clean sensory characteristics (e.g., high-purity Stevia Reb M 98%).
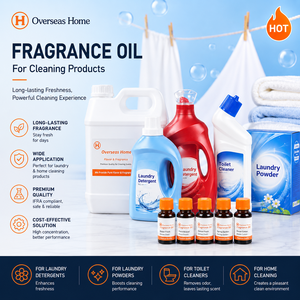
Relies on steam-distilled essential oils and concentrated floral fragrance oleoresins with long-lasting fixation performance, strict terpene profiles, and high batch-to-batch aromatic reproducibility.
To provide complete purchasing transparency, the following technical evaluations outline the processing methodologies, active marker benchmarks, and functional advantages across our primary export product catalog:
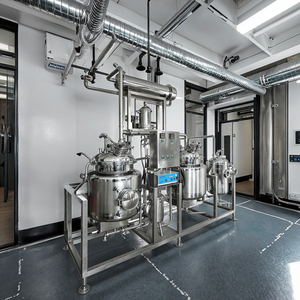
Modern extract manufacturing relies heavily on engineered hardware. Skid-mounted extraction and concentration equipment equipped with forced-circulation reflux condensers, vacuum concentrators, and integrated PLC control cabinets represent the backbone of scalable phytoprocessing. By utilizing SS304 or SS316L sanitary-grade contact surfaces, these systems maintain zero heavy metal leaching while optimizing solvent recovery (ethanol or water) at efficiency rates exceeding 95%.
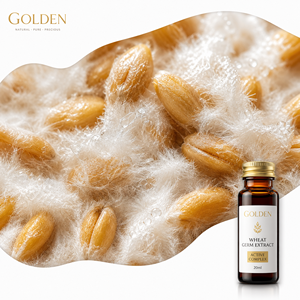
Concentrated Fermented Golden Mushroom Extract Liquid: Liquid-submerged fermentation technology breaks down rigid fungal cell walls, freeing high-molecular-weight beta-glucans and fungal polysaccharides. Bio-fermentation enhances the solubility and gut absorption profile compared to crude hot-water dried mushroom powders.
Industrial Fragrance Concentrates (Lavender & Vanilla): Solvent-free Supercritical Fluid Extraction (SFE) using liquid CO₂ isolates non-thermal botanical lipids and volatile terpenes without thermal degradation or chemical solvent residues (such as hexane or ethyl acetate). Ideal for clean-label cosmetics, premium soaps, and industrial laundry formulations.
| Extract Category | Extraction Technology | Primary Active Markers | Key Quality Control Metric | Target Sector |
|---|---|---|---|---|
| Pure Monomers | Chromatography & Recrystallization | Single compound ≥98% (Reb M, Crocetin) | HPLC Assay / Melting Point | Pharma & High-End Beverage |
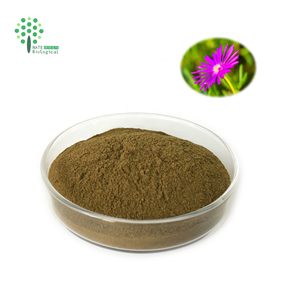
| Standardized Extracts | Ethanol/Water Hydro-Reflux | Target Bioactive Range (10:1 - 100:1) | UV-Vis / Heavy Metal Panel | Nutraceutical Capsules & Tablets |
| CO₂ Supercritical | Sub/Supercritical Liquid CO₂ | Lipids, Essential Oils, Oleoresins | GC-MS Terpene Profile / Zero Solvent | Softgels & Personal Care |
| Fermented Liquids | Submerged Liquid Fermentation | Fungal Polysaccharides / Peptides | Enzymatic Assay / Viscosity | Functional Food & Immunity Drinks |
As the botanical extraction industry advances, B2B procurement strategies are shifting from reactive purchasing to proactive risk mitigation and technical co-development. Suppliers must adapt to four pivotal technological trends shaping the global supply chain landscape:
Tightening global regulations regarding Class 2 and Class 3 residual solvents (ICH Q3C guidelines) have rendered traditional solvent extraction methods (such as benzene or chlorinated hydrocarbon systems) obsolete. The future belongs to Supercritical CO₂ Fluid Extraction (SFE) and Deep Eutectic Solvents (DES). CO₂ acts as a non-toxic, non-flammable, renewable solvent that leaves zero residue upon depressurization, making it the premier choice for organic-certified lipid fractions and essential oleoresins.
Advanced mass spectrometry (UHPLC-QTOF-MS) combined with artificial intelligence allows manufacturers to establish multi-dimensional chromatographic fingerprints for raw plant species. This prevents adulteration (such as synthetic dye additions or unlisted carrier spiking) and guarantees that every batch matches the bio-equivalence profile of the reference standard.
Global brand owners now demand full farm-to-factory transparency. RAAG Biotech manages contracted cultivation bases across key micro-climates, recording soil composition, harvest dates, pesticide application histories, and natural drying methods. Every finished drum is marked with an internal batch code traceable to specific farm coordinates.
Standard raw extract powders often present formulation challenges such as poor flowability, hygroscopicity, or low intestinal absorption. High-capacity suppliers are introducing micro-fluidization, spray drying with custom carrier matrices (such as non-GMO maltodextrin, rice starch, or gum arabic), and phospholipid complexation (e.g., Phytosome technology) to increase lipophilic compound absorption by up to 300%.
Selection of a long-term extraction partner depends on documented quality assurance systems. RAAG Biotech operates under strict cGMP protocols, ensuring every batch supplied to North American, European, and Asian markets meets rigorous international safety criteria.
Equipped with Waters HPLC systems, Agilent GC-MS equipment, UV-Vis spectrophotometers, and atomic absorption equipment for heavy metal testing (Pb, As, Cd, Hg).
Every shipment is accompanied by a batch-specific COA, MSDS, Technical Data Sheet (TDS), Allergen Statement, Non-GMO Certification, and Flow Chart.
Certified ISO 9001, ISO 22000, HACCP, HALAL, KOSHER, and USDA Organic compliant to streamline customs release and regulatory audits.
Connect directly with our technical sales engineers to request technical datasheets, full lot Certificate of Analysis records, or custom pilot batch quotes.